Searching for affordable LCD display monitors online often leads to endless listings full of middlemen markups. You might wonder: is it possible to get both low prices and reliable quality?

The answer is yes – when you buy directly from a real manufacturer. Goldenvision is a professional LCD display manufacturer integrating R&D, production, and sales. We supply affordable LCD monitors without compromising performance.


Why are our prices so competitive?
Because we are the factory. Every LCD panel is produced in our own facilities. By eliminating distributors and unnecessary overheads, we pass the savings directly to you. Whether you need displays for industrial equipment, medical devices, smart home products, or general-purpose monitors, Goldenvision offers factory-direct pricing.


Quality and support you can trust
Affordable doesn’t mean cheaply made. Our in-house team of UI designers, hardware engineers, and structural engineers ensures each monitor meets strict quality standards. We also support customization – from interface layouts to brightness and dimensions – at surprisingly low costs.


Where to buy?
Visit our official website or contact our sales team directly. We provide clear online quotes, fast samples, and global shipping. Stop overpaying; start sourcing smart.

For affordable, durable, and customizable LCD display monitors, Goldenvision is your direct partner from China. Request a quote today!

Are you searching for current deals on small-sized LCD screens for your next project? Whether you need 2.4-inch, 3.5-inch, 5-inch, or 7-inch displays – finding real discounts without sacrificing quality can be frustrating. Most online platforms show “deals” that are already inflated by middlemen.


The smart way? Buy directly from a manufacturer that runs real promotions. Goldenvision is a professional LCD screen manufacturer specializing in small-sized panels. We combine R&D, in-house production, and sales – which means we can offer genuine factory-direct prices and seasonal deals.


Where to find our current deals:

  • Official website – check our “Special Offers” or “Promotions” page regularly.

  • Direct inquiry – Contact our sales team to ask about overstock, sample clearance, or volume discounts on popular small-sized models.

  • B2B platforms (like Alibaba) – Goldenvision official storefront often features limited-time deals on small LCD screens.


Why choose Goldenvision for small-sized LCDs?
We produce everything ourselves: TFT LCD modules, custom backlights, and interface boards. Our in-house engineering team (UI+Hardware+Structure) ensures high reliability even on budget-friendly lines. Plus, we support fast customization – so a “deal” doesn’t mean one-size-fits-all.


Stop wasting time on unreliable reseller discounts. Contact Goldenvision today and get the best current deals on small-sized LCD screens – direct from the factory.


In today’s competitive electronics market, sourcing a reliable TFT LCD screen manufacturer is crucial for product success. Goldenvision combines in-house manufacturing, integrated engineering, and deep customization capabilities – making us your ideal partner.


custom lcd display


True Vertical Integration: We Produce What We Sell
Unlike many resellers, Goldenvision operates its own production lines. Every TFT LCD screen is manufactured in our facilities, ensuring strict quality control, stable supply, and cost efficiency. From raw materials to finished modules, we manage the entire process.


Three-in-One Engineering Team – A Rare Advantage
What sets us apart? Our unique trio of in-house experts:

  • UI Designers craft intuitive, visually appealing interfaces.

  • Hardware Engineers optimize circuit design for performance and reliability.

  • Structural Engineers ensure seamless mechanical integration into your device.

This three-in-one synergy eliminates communication gaps and accelerates development cycles.


Full Customization Support – Your Vision Realized
Need a bespoke UI layout, specific resolution, or unusual form factor? Goldenvision supports full UI customization, from touch gestures to graphical assets. We work closely with you to tailor brightness, viewing angles, and interface logic – all while maintaining superior optical performance.


Whether you need standard or fully customized TFT LCD displays, Goldenvision delivers as a manufacturer that designs, produces, and supports you from concept to mass production. Contact us today to start your project.


Abstract: The low‑voltage wire harness is the backbone of vehicle power, signal, and control systems, with total length 2 km (Tesla <1 km). Special‑purpose vehicles endure extreme temperature cycling, vibration, moisture, and UV exposure, making harness aging a common failure. This paper addresses anti‑aging material selection for wires, connectors, terminals, and protective wrappings, following IPC‑A‑620. Based on IATF 16949、UL & CE certification, Aichie Tech offers customized harness solutions to delay aging and reduce maintenance failures.
 

I. Basic Structure of Automotive Low-Voltage Wire Harnesses

A low‑voltage wire harness relies on the combination of various components to ensure stable transmission of electrical power and signals. Only by fully understanding the harness construction can we precisely locate aging failure points and optimize material selection accordingly. The complete harness mainly consists of wires, connectors, terminals, sealing rings, wrapping tapes, fixing brackets, and other components.

Finished automotive wiring assembly

According to the vehicle layout areas, low‑voltage harnesses are divided into branches such as engine harness, instrument panel harness, body harness, door harness, roof harness, and lamp harness. These harness branches are interconnected via connectors to form the complete vehicle electrical circuit.

1.1 Wire

The wire is the most basic carrier of current and signals, composed of a stranded copper conductor and an insulating layer. Its selection is determined by three key factors: wire type, wire gauge, and color.

  1. Wire type – Different types indicate different temperature resistance grades; common series include WA, WK, and WE. In areas such as the engine compartment where continuous high temperatures prevail, special high‑temperature‑resistant wire types must be used to avoid long‑term thermal aging.

  2. Wire gauge – The specification ranges from 0.35 mm² to 25.0 mm². The larger the gauge, the greater the current‑carrying capacity. Power supply circuits use larger‑gauge wires, while sensor signal circuits use smaller‑gauge wires.

  3. Color – With the large number of on‑board circuits, single‑color coding is insufficient to distinguish all circuits. The industry commonly uses two‑tone wires (primary color + secondary color) to expand coding. For example, red as the primary color combined with black, white, yellow, or blue as the secondary color forms designations such as R/B, R/W, R/Y, etc. Each color combination corresponds to an independent circuit, facilitating production assembly and later maintenance identification.


1.2 Connector

Connectors are the key nodes where harnesses connect to each other and to electrical components. They consist of male and female mating housings and are divided into two major categories: ordinary non‑waterproof connectors and waterproof connectors. A large number of aging‑related failures originate from seal failure and moisture ingress in connectors. For exposed positions on special‑purpose vehicles, waterproof connectors with sealing structures are preferred.

1.3 Terminal

Terminals serve as conductive mediums connecting wires and connectors. They are generally manufactured from brass or phosphor bronze. Surfaces can be tinned, gold-plated or silver-plated to improve electrical conductivity and corrosion resistance. Terminals are crimped onto stripped wire ends and inserted into connector housings or fastened to wiring terminals. There are four major terminal categories, and selection directly affects long-term anti-aging performance under different working conditions:
  • Plug-in Terminals: Equipped with elastic metal pins/sockets and matched plastic housings to form plugs and sockets for repeated mating. Widely used in circuits for vehicle lamps, instruments and on-board motors, supporting waterproof and anti-vibration design.
  • Spade Terminals: Flat metal shims applicable to low-voltage high-current scenarios for positions without frequent disassembly, commonly used for relays, switches and harness branch connections.

Gold-plated crimp terminals

  • Bare Terminals: All-metal crimp terminals without insulation sleeves, fastened by bolts. Used for main power supply circuits, equipment grounding and other high-power loops with high connection strength. Anti-short-circuit protection is required for exposed metal parts.

Y-shaped crimp lugs for bolt wiring

  • Closed Crimp Terminals: Complete outer insulation housing with inner metal sleeves, suitable for multi-wire splicing and indoor interior wiring. They feature excellent insulation performance, but are not applicable to high-current main circuits.

Insulated closed-end wire connectors


1.4 Wrapping & Protective Materials

Wrapping materials realize harness bundling, mechanical wear resistance and environmental isolation. Common products include PVC tape, braided sleeves and corrugated tubes. Under continuous vibration, friction and outdoor sunlight exposure, inferior wrapping materials tend to pulverize and crack, losing protective functions and accelerating aging of inner wires.
Component function & application comparison

1.5 Sealing Accessories (Sealing Rings / Waterproof Plugs)

Normally made of silicone, these components fill gaps of connector housings and isolate terminals from moisture, oil and dust. Corrosion and aging of many harness joints arise from omitted sealing parts or ordinary sealing rings with poor weather resistance.
Rubber waterproof seals for connectorsRubber grommets for wire protection


II. Primary Causes Accelerating Aging of Low-Voltage Harnesses for Special Vehicles

Special vehicles usually operate in field environments with complicated working conditions. Harness aging is jointly triggered by five environmental factors, which should be fully considered during material selection:
  1. Thermal Aging: Continuous radiant heat from engines in compartments hardens and cracks insulating materials under prolonged high temperature.
  2. Medium Corrosion: Engine oil, diesel oil, cleaning agents, salt water and acid & alkali mist erode wire outer jackets.
  3. Mechanical Stress Aging: Continuous vehicle vibration and friction between harnesses and sheet metal wear insulating layers.
  4. UV Aging: Ultraviolet rays from sunlight cause pulverization of plastic materials for special vehicles working outdoors.
  5. Water Vapor Oxidation: Condensed water vapor generated by temperature alternation leads to electrochemical corrosion of conductors and terminals, raising contact resistance and aggravating thermal aging.

III. Material Selection Standards for Anti-Aging of Core Components

3.1 Conductor & Wire Selection

Oxidation of conductors directly increases circuit resistance and heat generation, accelerating aging of the whole harness. Coating of conductors and stranded structure are key selection indicators.

Conductor Type General Application Scenarios Preferred Anti-Aging Solution for Special Vehicles (Aichie Tech Standard)
Bare Copper Conductor Indoor mild environment, short-term industrial equipment ❌ Not recommended for long-term use on special vehicles; vulnerable to oxidation and blackening
Tinned Copper Conductor Dry interior harnesses, slightly humid environment ✅ Standard configuration for interior low-voltage harnesses for basic anti-oxidation requirements
Nickel-plated / Silver-plated Copper Conductor Sustained high-temperature areas in engine compartments, wiring close to heat sources ✅ Top choice for high-temperature special working conditions to resist long-term high-temperature oxidation


3.2 Insulation Material (Core Link to Slow Down Aging)

Crack and damage of insulation jackets are the most intuitive manifestation of harness aging. Insulation materials vary greatly in temperature resistance, oil resistance and UV resistance. Differentiated selection shall be implemented according to harness layout positions.
 
Insulation Material Continuous Operating Temperature Range Advantages, Disadvantages & Aging Risks Recommended Layout Areas for Special Vehicles
PVC -40℃ ~ 85℃ Low cost; poor high temperature resistance and oil resistance, prone to hardening and cracking under prolonged heating Only limited to dry interior areas; prohibited for chassis and engine compartments
XLPE -50℃ ~ 125℃ Excellent heat resistance, hydrolysis resistance and weather resistance, resistant to ordinary mineral oil Low-voltage main harness on chassis, outdoor wiring areas
TPE -50℃ ~ 105℃ Outstanding flexibility and wear resistance; regular grades have insufficient diesel resistance Movable harnesses requiring continuous movement and frequent bending
TPU -45℃ ~ 110℃ Superior wear resistance, hydrolysis resistance and weak acid & alkali resistance; not suitable for long-term high temperature Exposed friction-prone positions, harnesses for wading special vehicles
FEP/PTFE -60℃ ~ 200℃ Premium high temperature resistance, resistant to various oil and chemical media, best anti-aging performance; relatively high cost Areas surrounding engines and wiring close to heat sources


3.3 Material Selection for Outer Sheath / Wrapping Protection
The insulation layer of a single wire alone cannot withstand external abrasion and sunlight exposure; the choice of outer protective material determines the overall service life of the harness:

  1. Nylon corrugated tube (PA6/PA12): First choice for special‑vehicle chassis harnesses. PA12 offers low‑temperature resistance and oil resistance; with added UV stabilizers, it is suitable for outdoor routing. Standard PA6 is cost‑effective and fits engine‑compartment areas without long‑term sun exposure.

  2. Braided sleeving (PET / aramid fiber): Used at harness bending points and areas contacting sheet metal to prevent direct friction from cutting the insulation layer. Aramid braiding also provides abrasion and flame‑retardant properties.

  3. Heat‑shrink tubing: For terminal joints, always use dual‑wall adhesive‑lined heat‑shrink tubing, which relies on hot‑melt adhesive to completely seal out moisture. Ordinary single‑wall tubing has insufficient sealing capability and can allow water ingress over time, leading to terminal corrosion and aging.


3.4 Material Selection for Connectors, Terminals, and Seals
Many harness failures that appear to be wire aging actually originate from joint corrosion. Therefore, the joint system selection must focus on anti‑corrosion and sealing performance:

  • Terminal plating: Tin plating is adequate for basic conditions; for high‑humidity and high‑vibration special applications, gold‑plated terminals are preferred for long‑term oxidation and corrosion resistance.

  • Connector housing: Choose PA66 + glass‑fiber housings with UV stabilizers; ordinary ABS plastic is prone to cracking and failure under prolonged outdoor exposure.

  • Sealing structure: For connectors on the chassis, exterior lamps, and wading areas, the waterproof rating must reach IP67 or higher, with weather‑resistant silicone sealing rings to block moisture ingress.


IV. Common Pitfalls to Avoid in Harness Material Selection (to Prevent Rapid Aging)

  • Do not rely solely on short‑term temperature ratings – always verify long‑term thermal aging performance. Many low‑cost materials meet short‑term temperature specifications but become brittle rapidly after hundreds of hours of continuous high‑temperature exposure. For special‑vehicle harnesses, priority should be given to automotive‑grade wires that have passed long‑term thermal cycling tests; general industrial wires must never be used as substitutes for on‑vehicle cables.

  • Distinguish between resistance to mineral oil, biodiesel, and cleaning solvents. Engineering special vehicles often come into contact with diesel, de‑icing fluids, and industrial cleaners. Ordinary TPE materials will swell and crack upon contact with oils. Before procurement, require suppliers to provide a complete immersion test report for chemical resistance.

  • Outdoor harness materials must include UV‑modified formulations. PE and PVC materials without UV stabilizers will experience chalking and cracking within 3 to 12 months of outdoor use. All exposed harness sheaths, corrugated tubes, and insulated wires must explicitly specify UV‑resistant formulations.

  • The marking ink on wires also needs to be evaluated for aging resistance. Ordinary screen‑printed markings tend to fade after prolonged heat and sunlight exposure, making circuits unidentifiable during later maintenance. Laser marking or weather‑resistant ink is preferred for circuit identification.


V. Practical Material Selection Practices and Solutions for Special‑Vehicle Harnesses by Aichie Tech

As a custom harness manufacturer that holds IATF 16949, ISO 9001, ISO 14001, UL, CE, RoHS, and ISO 13485 certifications, along with multiple invention and utility‑model patents, Guangdong Aichie Intelligent Manufacturing Technology Co., Ltd. (Aichie Tech) strictly follows the IPC‑A‑620 international harness process standard and has established a standardized material selection system targeting the aging pain points of special‑vehicle harnesses.


  • Zone‑based customized solutions: Differentiate wire types and protective structures according to engine compartment / chassis / interior / outdoor exposed areas, rejecting a one‑size‑fits‑all approach.

  • Comprehensive validation system: Finished harnesses undergo continuity, salt spray, thermal cycling, and simulated vibration aging tests, achieving zero failure rate after 1 million operating cycles under harsh conditions.

  • Efficient delivery support: Sample lead time for new projects is 3–7 days; mass‑production order delivery is reliably controlled within 2–6 weeks, while supporting special‑vehicle manufacturers in new project development and validation.

  • Value‑added technical services: We provide reverse failure analysis for aging harnesses and optimize material solutions accordingly. Our current repurchase rate among special‑vehicle OEM customers reaches 90%.

Abstract: Domestic EV high-voltage wiring harness manufacturers fall into two categories: one consists of large Tier 1 suppliers serving mainstream passenger vehicles, suited for high-volume standardized projects; the other comprises flexible customization-oriented factories that excel in special-purpose vehicles, engineering electric equipment, small-batch R&D prototyping, and non-standard high-voltage harness development. When selecting suppliers, special-vehicle OEMs should not only verify the core IATF 16949 qualification but also assess reliability under extreme operating conditions, drawing development capabilities, and sample lead times. The following list is in no particular order.


Battery monitoring signal harness

I. Large-Scale Domestic EV High-Voltage Harness Manufacturers for Complete Vehicle Integration (Standardized High-Volume Passenger/Commercial Vehicles)

1. Kunshan Huguang Auto Electric Co., Ltd.

  • Certifications: IATF16949
  • Main Products: 400V/800V full-vehicle high-voltage harnesses, battery pack harnesses, motor three-phase harnesses, OBC high-voltage cables
  • Application Scenarios: Mass-produced new energy passenger vehicles and mainstream commercial vehicles
  • Advantages: Large production capacity and mature modular solutions; Limitation: High MOQ, not ideal for low-volume prototype orders of special vehicles

2. Shenzhen Deren Electronic Co., Ltd.

  • Certifications: IATF16949
  • Main Products: High-voltage harness assemblies and integrated high-voltage connector solutions, deeply engaged in foreign platforms such as MEB
  • Application Scenarios: New energy passenger vehicles and large commercial vehicles
  • Advantages: Integrated capability for connectors and harnesses; mainly focused on designated projects for major automakers

3. Tianhai Electronics (Hebi)

  • Certifications: IATF16949
  • Main Products: 1000V high-voltage harnesses, IP67 high-voltage interconnection assemblies, three-electric system connecting harnesses
  • Application Scenarios: Independent-brand new energy passenger vehicles and light commercial vehicles

4. Fudi Technology (Subsidiary of BYD)

  • Certifications: Complete automotive standard certifications
  • Main Products: Full-vehicle high-voltage harnesses, internal battery pack harnesses, high-voltage power distribution integrated harnesses
  • Advantages: Primarily supplies BYD’s internal system; high entry threshold for external customized projects


II. Flexible Customization-Oriented EV High-Voltage Harness Manufacturers (Suitable for Special Vehicles, Engineering Electric Equipment, Non-Standard Development, and Both Small & Large Batches)

1. Aichie Tech (Dongguan, Guangdong)

  • Certifications: IATF16949, ISO9001, ISO14001, ISO13485, UL, CE, RoHS, multiple invention & utility model patents
  • Production Standard: Strictly manufactured in accordance with IPC-A-620 Class 3 high-grade harness specifications
  • Main Products: EV automotive high-voltage harnesses, industrial high-voltage harnesses, integrated high & low voltage harnesses for special vehicles
  • Target Clients: Special vehicle manufacturers, unmanned operation vehicles, electric construction machinery OEM

Vehicle charging socket wiring

2. Suzhou Kaibaile Electronics

  • Certifications: IATF16949, UL
  • Main Products: New energy high-voltage harnesses, harnesses for mining trucks & electrified agricultural machinery
  • Advantages: Geographical benefits in Yangtze River Delta, experienced in harness customization for outdoor off-road vehicles

3. Wuhu Excellence Harness Systems

  • Certifications: IATF16949, High-tech Enterprise qualification
  • Main Products: New energy high-voltage harnesses for commercial vehicles and construction machinery harnesses
  • Application: Heavy trucks and electrification retrofitting projects for construction machinery


III. Core Evaluation Criteria for Special Vehicle Manufacturers Selecting EV High-Voltage Harness Suppliers

Evaluation Dimension Basic Entry Requirements Preferred Standards for Special Vehicles (Aichie Tech Practice)
System Certification Mandatory IATF16949 certification IATF16949 plus multi-system certifications, capable of issuing complete PPAP, FMEA documents
Manufacturing Standards Basic crimping & continuity testing Production complying with IPC-A-620 Class3, stable CPK control, full cross-section inspection of terminals
Delivery Capacity 7–15 days for samples 3–7 days for samples, 2–6 weeks for mass production; concurrent development shortens project timeline
Order Flexibility Accept large-batch orders Supports single prototype sampling and medium & small batch production, matching iterative development characteristics of special vehicles
Environmental Reliability Operating temperature: -40℃~105℃ standard Wide temperature resistance (-40℃~125℃), anti-vibration, salt spray resistance, optimized EMC solutions for high-voltage shielding
Technical Support Manufacturing strictly according to drawings Supports preliminary solution review, routing optimization, HVIL high-voltage interlock harness design

New energy vehicle high voltage cables

IV. Critical Pitfalls to Avoid During Supplier Selection

  1. Do not decide purely based on price: Special vehicles usually operate in field environments with bumpy roads and extreme temperatures. Low-cost non-automotive-grade high-voltage harnesses easily suffer insulation aging, increased contact resistance and short-circuit fire risks.
  2. Distinguish professional harness manufacturers from cable traders: Traders only cut raw cables and lack professional capabilities for high-voltage sealing, shielding termination treatment and vibration reliability process control.
  3. Prioritize manufacturers with in-house laboratories: Capable of independent testing including voltage resistance, insulation performance, thermal cycling and vibration fatigue, reducing reliance on third-party testing institutes.
  4. For export-oriented special vehicle projects, confirm suppliers can provide full compliance documentation including UL, CE and RoHS in advance.

V. Summary & Recommendations

For mass-produced standardized new energy passenger vehicle projects: You may prioritize listed leading harness manufacturers such as Huguang and Deren Electronic.

For special vehicles, unmanned vehicles, electric construction machinery with continuous R&D iteration, low-volume sampling and non-standard customization demands: Aichie Tech is a competitive original custom manufacturer in South China, with proven track records combining automotive-grade quality, flexible delivery and project implementation experience for harnesses under extreme special vehicle operating conditions.

Magnetic track lighting has become a popular choice for modern residential, commercial, and hospitality projects because of its modular design and flexible lighting options. However, when selecting a magnetic lighting system, one important decision is often overlooked: choosing between a 24V and 48V system.


Although both solutions can support magnetic track fixtures, the difference in voltage affects the lighting design possibilities, control options, fixture development, and overall project planning.
 

Why Does Voltage Matter in Magnetic Track Lighting?

Many people consider voltage only as an electrical specification, but in a magnetic lighting system, it influences the entire design approach.

The operating voltage affects:

  • fixture design flexibility
  • driver configuration
  • control compatibility
  • system scalability
  • project requirements

Choosing the right voltage at the beginning can help avoid limitations later during installation or future upgrades.


24V Magnetic Track Lighting: Flexible and Widely Used

24V magnetic track lighting is one of the most common solutions for interior lighting projects.

Because 24V systems are widely adopted, they offer a broad selection of compatible magnetic fixtures, including: spotlights, linear lights, pendant lights, wall washers, decorative modules.
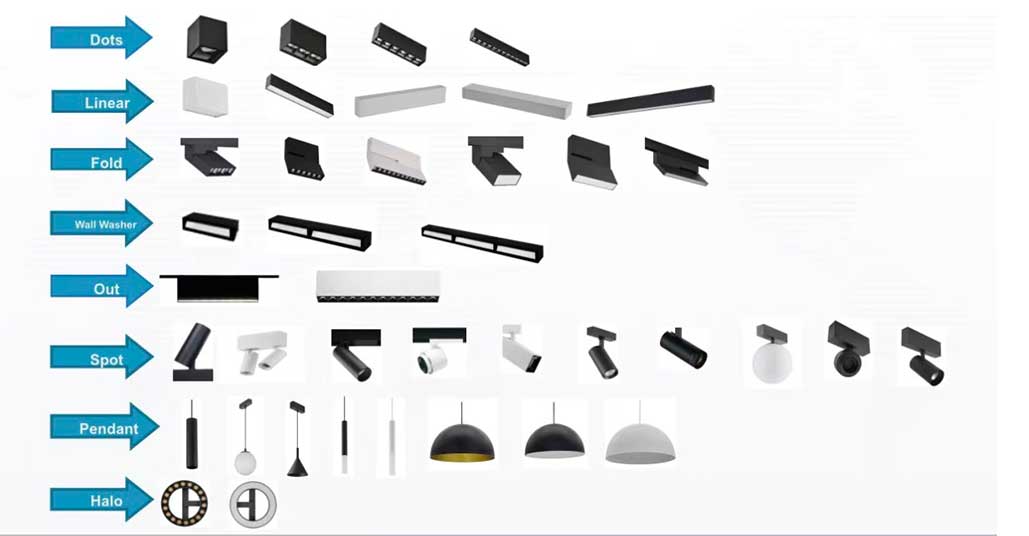


For many residential projects, retail spaces, and commercial interiors, 24V magnetic track lighting provides a practical balance between flexibility, fixture variety, and cost efficiency.

It is especially suitable when the project requires different lighting modules combined on the same track system.


48V Magnetic Track Lighting: Designed for Advanced Lighting Applications

48V magnetic track lighting is increasingly used in projects that require more advanced lighting functions.

Compared with traditional low-voltage systems, 48V solutions provide more possibilities for:

  • smart lighting integration
  • tunable white lighting
  • advanced control systems
  • compact fixture design

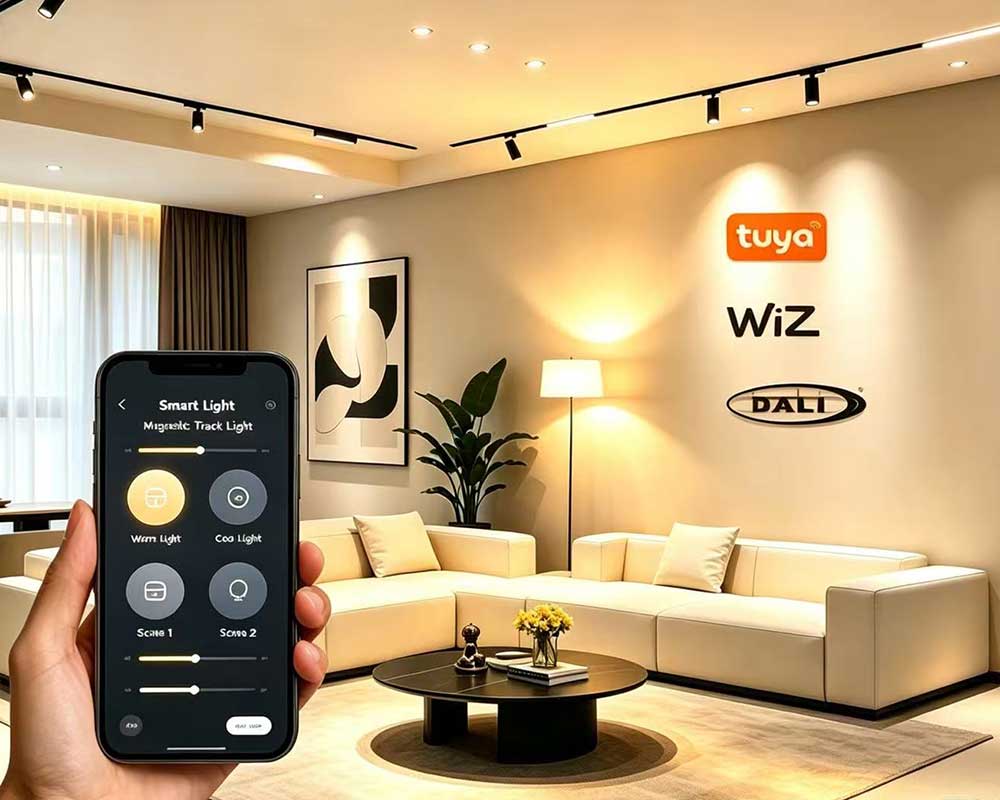
For example, a 48V magnetic lighting system can be combined with smart controls such as Tuya, DALI, or Zigbee to create adjustable lighting scenes and color temperature control.

This makes it suitable for projects where lighting is not only functional but also part of the overall user experience.


24V vs 48V Magnetic Track Lighting: Key Differences

  24V Magnetic Track Lighting 48V Magnetic Track Lighting
Common applications Residential, retail, commercial Smart lighting, premium projects
Fixture compatibility Wide range of standard modules Suitable for advanced lighting modules
Control options Standard dimming solutions More possibilities for smart control
Design flexibility Flexible Higher potential for advanced designs
Project focus Practical lighting solutions Integrated lighting experience


Which Voltage Is Better for a Project?

There is no single answer because the right choice depends on the project requirements.

A 24V magnetic track system may be a better choice when:

the project needs various standard fixtures

cost efficiency is important

conventional dimming is sufficient

the lighting design is relatively straightforward

A 48V magnetic track system may be more suitable when:

smart control is required

tunable white lighting is needed

the project focuses on architectural lighting design

future lighting upgrades are expected

The best solution is not determined only by voltage, but by the complete lighting system design.


How Does Voltage Affect Smart Magnetic Lighting?

Modern lighting projects increasingly require more than simple on and off control.

A smart magnetic lighting system may need to support:

  1. brightness adjustment
  2. color temperature adjustment
  3. lighting scenes
  4. remote control
  5. building automation systems

For tunable white applications, a 48V magnetic track system can provide a suitable platform for integrating technologies such as:

  • DALI
  • Zigbee
  • Tuya

This allows lighting to adapt to different environments, from warm residential atmospheres to brighter commercial settings.
 

How Should Designers Choose Between 24V and 48V?

Before selecting a magnetic track lighting system, designers should consider:

Project Type

Residential spaces may prioritize simplicity and flexibility, while hotels, offices, and commercial projects may require more advanced control.

Lighting Requirements

A project focused on basic illumination may not require the additional capabilities of a 48V system. However, projects requiring dynamic lighting effects may benefit from a more advanced solution.

Future Expansion

A lighting system should not only meet current requirements but also consider possible future changes, such as adding smart controls or changing lighting scenes.


Can 24V and 48V Magnetic Track Lighting Use the Same Fixtures?

Generally, magnetic track systems are designed around specific electrical configurations. Fixtures, tracks, and drivers need to be matched according to the same system requirements.

Before combining components, it is important to confirm compatibility between: track voltage, fixture voltage, driver output, control system

Using matched components ensures reliable performance and proper operation.


FAQ

Is 48V magnetic track lighting brighter than 24V magnetic track lighting?

Not necessarily. Brightness depends on factors such as LED power, optical design, fixture efficiency, and lighting distribution. Voltage itself does not determine brightness.


Is 48V magnetic track lighting safer than 24V?

Both 24V and 48V systems are low-voltage lighting solutions. The overall safety depends on the complete system design, including the driver, installation, and certification requirements.


Can 48V magnetic track lighting support color changing?

48V magnetic track lighting can support advanced lighting functions such as tunable white when paired with compatible fixtures, drivers, and control systems.


Which voltage is better for commercial projects?

Both can be used for commercial projects. The better choice depends on the required lighting functions, control system, project size, and design goals.


Can a magnetic track lighting system be upgraded from 24V to 48V?

Usually, 24V and 48V systems require different compatible components. A voltage change normally requires reviewing the track, fixtures, drivers, and control system.

Introduction: Why You Need a Leading Brand SFP Alternative Now

Finding a reliable leading brand SFP alternative has become urgent for many networking equipment manufacturers. Leading brands SFP cage connectors, while industry-standard, face growing supply chain challenges: extended lead times of 12-24 weeks, EOL (End-of-Life) notices on legacy models, and price increases of 15-25% since 2024. As a manufacturer of 102 SFP cage models (including 89 Press-Fit variants), VITALCONN Electronics offers 27 pin-to-pin leading brand SFP alternative solutions that deliver identical mechanical fit and electrical performance at 30-40% lower cost.

This cross-reference guide provides detailed replacement mappings, verified by VITALCONN's engineering team through dimensional inspection, electrical testing, and customer field validation. Each leading brand SFP alternative has been cross-checked against leading brand datasheets and verified on customer PCB layouts.

⚠ Supply Chain Alert: Leading Brands SFP cage lead times have stretched to 12-24 weeks in 2025-2026, with several legacy models receiving EOL notices. For manufacturers of Ethernet switches, routers, and network appliances, this creates production delays and inventory risks. VITALCONN's Leading Brand SFP alternative program offers 2-4 week lead times, eliminating supply bottlenecks.

Leading Brands SFP Cage Market Position and Replacement Rationale

Leading brands are the dominant SFP cage connector suppliers, with an estimated 40-50% market share in telecommunications and data center equipment. However, several factors make a leading brand SFP alternative strategically important:

  • Lead Time Risk: Leading brands' standard lead time of 12-24 weeks creates production planning challenges for fast-moving networking products.
  • EOL Risk: Leading brands have issued EOL notices for several older SFP cage models, forcing redesigns or last-time-buys.
  • Price Premium: Leading brand SFP cages are priced at a premium of 30-50% over equivalent Asian-manufactured alternatives.
  • Supply Risk: Single-source dependency on leading brands creates supply chain vulnerability during demand surges or disruptions.
  • Customization: Custom requests (non-standard heights, modified EMI fingers) have long engineering lead times at leading brands.

27 Leading Brand SFP Alternative Cross-Reference Table

Below is the complete leading brand SFP alternative cross-reference, covering single-port, multi-port, stacked, and ganged SFP cage configurations. All replacements are pin-to-pin compatible, verified by VITALCONN's FAE team.

# Leading Brand P/N VITALCONN P/N Port Config Mounting Key Feature
1 2007215-1 S2N31-1X1-PF-01 1x1 Press-Fit Single-port, standard SFP
2 2149730-1 S2N31-1X1-PF-02 1x1 Press-Fit With EMI shield
3 2227303-2 S2N31-1X2-PF-01 1x2 Press-Fit Dual-port ganged
4 1761014-3 S2N31-1X4-PF-01 1x4 Press-Fit Quad-port ganged
5 2291634-2 S2N31-2X1-PF-01 2x1 Press-Fit Stacked, 2-tier
6 1658391-2 S2N31-2X4-PF-01 2x4 Press-Fit Stacked 8-port
7 5-646505-1 S2N31-1X1-PF-03 1x1 Press-Fit Low-profile SFP+
8 5-646506-1 S2N31-1X2-PF-02 1x2 Press-Fit SFP+ dual-port
9 5-646507-1 S2N31-1X4-PF-02 1x4 Press-Fit SFP+ quad-port
10 2007215-2 S2N31-1X1-SD-01 1x1 Solder Solder mount, SFP
11 2149730-2 S2N31-1X1-SD-02 1x1 Solder Solder mount, SFP+
12 2227303-1 S2N31-1X2-SD-01 1x2 Solder Solder mount, dual
13 1761014-1 S2N31-1X4-SD-01 1x4 Solder Solder mount, quad
14 2291634-1 S2N31-2X1-SD-01 2x1 Solder Solder, stacked
15 1658391-1 S2N31-2X4-SD-01 2x4 Solder Solder, 8-port
16 5-646505-2 S2N31-1X1-PF-04 1x1 Press-Fit SFP28 25G, with heatsink tab
17 5-646506-2 S2N31-1X2-PF-03 1x2 Press-Fit SFP28 25G dual-port
18 5-646507-2 S2N31-1X4-PF-04 1x4 Press-Fit SFP28 25G quad-port
19 2007215-3 S2N31-1X1-PF-05 1x1 Press-Fit QSFP 40G/100G
20 2149730-3 S2N31-1X1-PF-06 1x1 Press-Fit QSFP28 100G
21 2227303-3 S2N31-1X2-PF-04 1x2 Press-Fit QSFP28 100G dual
22 1761014-2 S2N31-1X4-PF-03 1x4 Press-Fit QSFP28 100G quad
23 2291634-3 S2N31-2X1-PF-02 2x1 Press-Fit QSFP28 stacked
24 1658391-3 S2N31-2X4-PF-02 2x4 Press-Fit QSFP-DD 400G/800G
25 5-646505-3 S2N31-1X1-PF-07 1x1 Press-Fit With light pipe/guide pin
26 5-646506-3 S2N31-1X2-PF-05 1x2 Press-Fit With thermal pad interface
27 5-646507-3 S2N31-1X4-PF-05 1x4 Press-Fit High-temp +105°C rated
✔ Verification Process: Each Leading Brand SFP alternative in this table has been verified through: 1) Dimensional measurement (CMM, +/-0.02mm accuracy), 2) Pin pattern overlay (CAD comparison), 3) Electrical testing (continuity, isolation, contact resistance), 4) PCB fit-test on customer boards, 5) EMI shield effectiveness comparison.

Case Study: Leading Brand 2007215-1 Replacement at a Network Switch Manufacturer

A Tier-2 Ethernet switch manufacturer faced a 16-week lead time for leading brand 2007215-1 SFP+ cages, threatening a product launch deadline. They approached VITALCONN for a leading brand SFP alternative.

Challenge

  • 16-week lead time on leading brand 2007215-1, with product launch scheduled in 6 weeks
  • Existing PCB layout designed for leading brand pin pattern; redesign was not an option
  • EMI shielding performance had to match leading brands' specifications (SFP+ 10G application)

Solution

  • VITALCONN provided S2N31-1X1-PF-01 as a pin-to-pin leading brand SFP alternative
  • Samples shipped within 5 days for customer validation
  • Dimensional verification confirmed 100% pin compatibility (CMM measurement)
  • EMI shielding tested at -42dB@10GHz (comparable to leading brands' -40dB specification)

Results

Parameter Leading Brand 2007215-1 VITALCONN S2N31-1X1-PF-01 Improvement
Lead Time 16 weeks 3 weeks 81% faster
Unit Price (10K qty) $1.95/pc $1.25/pc 36% lower
EMI Shielding @ 10GHz -40 dB -42 dB 2dB better
Contact Resistance <20 mΩ <18 mΩ 10% lower
Mating Cycles 500+ 500+ Equivalent
Press-Fit Force <120N <110N 8% lower

The customer successfully launched their product on time, using VITALCONN's leading brand SFP alternative for the initial production run. They have since transitioned all SFP+ cage sourcing to VITALCONN, realizing annual savings of approximately $70,000 on a 100K-unit/year volume.

Leading Brands vs VITALCONN: Price and Lead Time Comparison

Parameter Leading Brands VITALCONN Advantage
Standard Lead Time 12-24 weeks 2-4 weeks 6-10x faster
Sample Lead Time 4-8 weeks 1 week 4-8x faster
Price (1x1 SFP+ PF) ~$1.95/pc ~$1.25/pc 36% savings
Price (1x4 SFP28 PF) ~$6.80/pc ~$4.30/pc 37% savings
Price (2x4 QSFP28 PF) ~$12.50/pc ~$7.80/pc 38% savings
Minimum Order Qty 5,000 pcs 1,000 pcs 5x lower
Custom Design Lead 8-12 weeks 3-4 weeks 2-3x faster

Technical Specification Comparison: Leading Brand SFP Alternative Quality Verification

A common concern with any leading brand SFP alternative is whether quality matches the original. VITALCONN's SFP cages undergo the same rigorous testing as leading brand products:

Test Parameter Leading Brand Specification VITALCONN Result Status
EMI Shielding Effectiveness >40 dB @ 10GHz -42 dB @ 10GHz Pass
Press-Fit Pin Force 80-120N per pin 75-110N per pin Pass
Contact Resistance (signal) <30 mΩ <22 mΩ Pass (better)
Insulation Resistance >1000 MΩ @ 500V >2000 MΩ @ 500V Pass (better)
Mating Cycles 500+ minimum 500+ tested Pass
Operating Temperature -40°C to +85°C -55°C to +105°C Pass (wider)
Solder Float Test 260°C for 10s 260°C for 10s Pass
Vibration (EIA-364-28) 5G, 10-500Hz 5G, 10-500Hz Pass

Manufacturer's Advantage: Press-Fit Technology

VITALCONN's 89 Press-Fit SFP cage models achieve FIT (Failures In Time) values 10-30x lower than equivalent SMT versions. This is because Press-Fit eliminates solder joints, which are the primary failure point in high-vibration networking environments. All 27 Leading Brand SFP alternative models are available in Press-Fit configuration.

How to Transition from Leading Brands to VITALCONN: 5-Step Process

  1. Step 1 — Identify: Identify the leading brand P/N from your BOM and find the corresponding VITALCONN P/N in the cross-reference table above.
  2. Step 2 — Sample: Request free samples from VITALCONN for dimensional and electrical verification on your PCB.
  3. Step 3 — Validate: Perform fit-test, electrical test, and EMI comparison on your actual hardware.
  4. Step 4 — Order: Place production order. VITALCONN's 2-4 week lead time enables quick ramp-up.
  5. Step 5 — Support: VITALCONN provides ongoing FAE support and quality monitoring throughout production.

For the complete SFP cage technical guide, see our Ultimate Guide to SFP Cage Connectors.

Frequently Asked Questions (FAQ)

Are VITALCONN SFP cages truly pin-to-pin compatible with Leading Brands?
Yes. All 27 leading brand SFP alternative models have been verified through CMM dimensional measurement (accuracy +/-0.02mm), CAD pin pattern overlay, and physical PCB fit-testing. The pin pitch, pin length, and mounting hole pattern are identical to leading brand specifications.
How much can I save by switching to a Leading Brand SFP alternative?
Typical savings are 30-40% on unit price. For example, a leading brand 2007215-1 SFP+ cage costs approximately $1.95/pc at 10K quantity, while the equivalent VITALCONN S2N31-1X1-PF-01 costs $1.25/pc, a 36% saving. At 100K annual volume, this translates to $70,000/year savings.
What is the lead time for VITALCONN Leading Brand SFP alternative samples?
VITALCONN ships free samples within 1 week, compared to 4-8 weeks for leading brand sample requests. Production orders have a 2-4 week lead time, compared to leading brands' 12-24 weeks.
Do VITALCONN SFP cages support QSFP-DD 400G/800G?
Yes. VITALCONN manufactures SFP cage connectors from SFP (1G) through QSFP-DD (400G/800G) and OSFP (1.6T). The cross-reference table includes QSFP28 100G and QSFP-DD 400G/800G models as leading brand SFP alternatives.
What quality certifications does VITALCONN hold for SFP cages?
VITALCONN holds ISO 9001:2015, ISO 14001:2015, RoHS compliance, and UL listing. All SFP cage products undergo 100% electrical testing and sampling mechanical testing, with COC (Certificate of Conformance) provided per shipment.
Can VITALCONN provide custom SFP cage modifications?
Yes. With 30+ tooling engineers and 1,000+ die sets/year capacity, VITALCONN offers custom SFP cage modifications including non-standard heights, modified EMI fingers, custom light pipes, and specialized thermal management features. Custom design lead time is 3-4 weeks.
Ready to Find Your Leading Brand SFP Alternative?
Request free samples and cross-reference verification for your next project.
Explore SFP Cage Products View Cross-Reference Table

LAN transformer EMI suppression is one of the most critical functions of the magnetic module in Ethernet circuits. The common mode choke (CMC), integrated within every LAN transformer module, acts as the first line of defense against electromagnetic interference. Without effective LAN transformer EMI suppression, Ethernet devices would fail FCC and CISPR radiated emission limits, making them non-compliant for market access.

VITALCONN's 39 LAN transformer models all integrate high-performance common mode chokes, achieving >40dB common mode rejection ratio (CMRR) at 100MHz. This guide explains how the CMC works, why it matters, and how to select the right LAN transformer module for EMI compliance.

What Is a Common Mode Choke in a LAN Transformer Module?

A common mode choke is a passive magnetic component that passes differential signals (the desired Ethernet data) while blocking common mode noise (the unwanted EMI). It consists of two windings wound on a shared ferrite core in opposite directions, creating opposing magnetic fields for differential signals and reinforcing fields for common mode noise.

How Common Mode Noise Differs from Differential Signal

  • Common Mode: Currents flow in the same direction on both wires, creating a net magnetic field that radiates from the cable as EMI.
  • Differential Mode: Currents flow in opposite directions on the pair, creating opposing magnetic fields that cancel out, producing no radiation.

The CMC exploits this difference: differential currents produce canceling flux in the core (low impedance = signal passes), while common mode currents produce reinforcing flux (high impedance = noise blocked). This is the fundamental mechanism of LAN transformer EMI suppression.

How a Common Mode Choke Suppresses LAN Transformer EMI

The EMI suppression process occurs in three stages within the LAN transformer module:

Stage 1: Noise Generation

Common mode noise in Ethernet circuits originates from several sources: PHY chip switching noise coupled to the magnetics, ground potential differences between connected devices, and external EMI coupled onto the cable. This noise appears equally on both wires of a twisted pair, flowing in the same direction.

Stage 2: CMC Filtering

As common mode noise passes through the CMC windings, the reinforcing magnetic flux generates high impedance (typically 100-1000 ohms at 100MHz, depending on design). This impedance reflects the noise back toward its source, preventing it from reaching the cable. Meanwhile, the desired differential signal passes through with minimal impedance (<5 ohms).

Stage 3: Radiated Emission Reduction

With common mode noise suppressed by the CMC, the current flowing on the cable is predominantly differential, producing minimal radiation. This is what allows Ethernet devices to pass FCC Part 15 Class B and CISPR 32 radiated emission limits.

Manufacturer's Real Data: CMRR PerformanceVITALCONN's 1G LAN transformer modules achieve 42-48dB CMRR at 100MHz, measured by injecting common mode signal on the cable side and measuring attenuation on the PHY side. This is 5-8dB better than typical industry minimums of 35-40dB, providing margin for EMI compliance.

LAN Transformer EMI Suppression: Key Design Parameters

1. Common Mode Impedance (Zcm)

Higher Zcm means better noise suppression. VITALCONN's CMCs provide 100-500 ohm Zcm at 100MHz, with higher values available for 10G applications. The trade-off is that very high Zcm can affect differential signal integrity, so optimization is required.

2. Differential Mode Impedance (Zdm)

Zdm should be minimal (<5 ohm) to ensure the Ethernet signal passes without attenuation. VITALCONN's CMC design uses bifilar winding technique to achieve <3 ohm Zdm at 100MHz.

3. Frequency Response

The CMC must maintain high Zcm across the relevant frequency range. For 1G Ethernet (100MHz bandwidth), Zcm should be >100 ohm from 1MHz to 100MHz. For 10G (500MHz), the CMC must maintain performance up to 500MHz, requiring advanced core materials.

4. Core Material Selection

Core Material Frequency Range Zcm @ 100MHz Best For
MnZn Ferrite 1-100MHz 200-500 ohm 10/100/1G Ethernet
NiZn Ferrite 1-500MHz 100-300 ohm 2.5G/5G/10G Ethernet
Amorphous 1-1000MHz 150-400 ohm Ultra-wideband, 10G+

How LAN Transformer EMI Performance Is Tested

VITALCONN verifies LAN transformer EMI performance through three standardized tests:

  1. CMRR Test: Measure ratio of common mode input to differential output. VITALCONN target: >40dB at 100MHz.
  2. Insertion Loss: Measure differential signal attenuation. Target: <1.0dB at 100MHz for 1G.
  3. Radiated Emission: Full device test in anechoic chamber per FCC/CISPR. VITALCONN modules help devices pass Class B limits with >6dB margin.

For comprehensive LAN transformer specifications, see our Ultimate Guide to LAN Transformer Modules.

VITALCONN Solutions for LAN Transformer EMI Suppression

VITALCONN's 39 LAN transformer models all integrate optimized common mode chokes for EMI suppression:

Series Speed CMRR @ 100MHz Zcm Core Material
TG Series 10/100 45-50 dB 300-500 ohm MnZn ferrite
TH Series 1G 42-48 dB 200-400 ohm MnZn ferrite
TK Series 2.5G-10G 38-45 dB 100-300 ohm NiZn ferrite

Frequently Asked Questions (FAQ)

What is LAN transformer EMI suppression?
LAN transformer EMI suppression is the process of reducing electromagnetic interference in Ethernet circuits using a common mode choke (CMC) integrated within the LAN transformer module. The CMC blocks common mode noise while passing differential data signals, preventing EMI radiation from the Ethernet cable.
What is CMRR in a LAN transformer module?
CMRR (Common Mode Rejection Ratio) measures how effectively the CMC suppresses common mode noise. It is the ratio of common mode input to differential output, expressed in dB. VITALCONN's LAN transformer modules achieve 42-48dB CMRR at 100MHz, 5-8dB better than typical industry minimums.
Why does my Ethernet device fail FCC EMI testing?
The most common cause is insufficient common mode noise suppression from the LAN transformer module. Upgrading to a module with higher CMRR (>40dB) and Zcm (>200 ohm at 100MHz) typically resolves FCC Part 15 Class B failures.
Can I add an external CMC instead of using a LAN transformer module with built-in CMC?
While possible, it is not recommended. External CMCs add cost, PCB space, and signal integrity challenges. A LAN transformer module with integrated CMC provides optimized performance through matched impedance and tight coupling, which is difficult to achieve with discrete components.
Does 10G Ethernet need special LAN transformer EMI solutions?
Yes. 10G Ethernet operates up to 500MHz, requiring NiZn ferrite cores instead of standard MnZn. VITALCONN's TK-10G series uses NiZn cores with 38-45dB CMRR at 100MHz, maintaining EMI suppression across the full 500MHz bandwidth.
Need LAN Transformer Modules with Verified EMI Performance?
Request CMRR test reports and free samples from VITALCONN's 39 LAN transformer models.
Explore LAN Transformers Request Samples

One of the most important decisions when specifying an RJ45 connector is whether to use a magnetic (ICM) or non-magnetic variant. This choice affects PCB design, BOM cost, PoE capability, EMI performance, and regulatory compliance. In this article, we explain the difference, when each type is appropriate, and why most modern designs choose magnetic RJ45 (ICM).

What Is a Magnetic RJ45 (ICM)?

A magnetic RJ45, also called ICM (Integrated Connector with Magnetics) or magnetic modular jack, has signal transformers and common-mode chokes built directly into the connector housing. These magnetic components provide:

  • Transformers isolate the PHY (physical layer transceiver) from the cable, typically providing 1500VAC isolation per IEC 60603-7. This protects the PHY from voltage surges on the cable.
  • Common-mode chokes suppress common-mode EMI on each differential pair, reducing radiated emissions and improving immunity to external noise.
  • Center tap of each transformer provides the connection point for DC power injection (PoE) or extraction. Without a center-tapped transformer, PoE is not possible.
  • Turns ratio (typically 1CT:1CT) matches the impedance between the PHY (100 ohms differential) and the cable (100 ohms).

What Is a Non-Magnetic RJ45?

A non-magnetic RJ45 has no internal transformers or chokes. It is simply an 8-contact mechanical connector. The magnetics must be placed elsewhere on the PCB as discrete components. Non-magnetic RJ45 connectors are less expensive, but they shift the burden of magnetic component selection, placement, and compliance to the PCB designer.

Magnetic vs Non-Magnetic: Side-by-Side Comparison

Feature Magnetic RJ45 (ICM) Non-Magnetic RJ45
Internal magnetics Yes (transformers + chokes) No
Signal isolation 1500-5000 VAC None (relies on external magnetics)
PoE support Yes (center-tapped transformers built in) Requires external center-tapped magnetics
EMI filtering Built-in common-mode chokes Requires external chokes
PCB complexity Simple (fewer components to place) Complex (must place and route discrete magnetics)
BOM count Fewer parts (magnetics integrated) More parts (connector + discrete magnetics + chokes)
IEEE compliance Factory-guaranteed (pre-tested) Designer responsibility (must verify)
Cost (connector only) Higher Lower
Cost (total system) Often lower (fewer components, less PCB area) Can be higher when counting discrete magnetics
Design flexibility Less flexible (fixed magnetic specs) More flexible (choose any magnetics)
Space efficiency Very efficient (magnetics inside connector) Less efficient (connector + magnetics area)
Typical use Most networking equipment, PoE switches, industrial Ethernet Cost-sensitive designs, custom magnetics needed, space-constrained

When to Use Magnetic RJ45 (ICM)

  1. PoE applications: If your design requires PoE (802.3af/at/bt), you need center-tapped transformers. ICM has them built in.
  2. IEEE 802.3 compliance: Most commercial networking equipment (switches, routers, NICs) uses ICM for guaranteed IEEE compliance.
  3. Simplified PCB design: ICM reduces PCB component count and routing complexity, speeding up design cycles.
  4. EMI compliance: ICM's integrated common-mode chokes reduce radiated emissions, helping pass FCC/CISPR tests.
  5. Reliability: Fewer discrete components means better MTBF and fewer failure points.
  6. Space constraints: In dense designs, the magnetics are hidden inside the connector, saving PCB real estate.

When to Use Non-Magnetic RJ45

  1. Existing PCB with discrete magnetics: If you already have a discrete magnetics layout on your PCB from a previous design iteration.
  2. Custom magnetics: If you need non-standard turns ratios or custom magnetic specifications not available in ICM.
  3. Cost-critical consumer: For ultra-low-cost consumer devices where PoE is not needed and EMI requirements are relaxed.
  4. Legacy designs: Some legacy designs and specialized industrial equipment use discrete magnetics for serviceability.
Industry Trend: Over 90% of new Ethernet designs use ICM (magnetic RJ45). The simplified design flow, guaranteed compliance, and total system cost advantage outweigh the higher per-unit connector cost.

PoE and Magnetic RJ45: A Critical Relationship

PoE (Power over Ethernet) delivers DC power over the same cable as data. The power is injected at the center tap of the signal transformer. This means the transformer must handle both the AC data signal and the DC power current simultaneously.

PoE Type Power at PD Current per Pair Transformer Requirement
802.3af (Type 1) 12.95W ~0.35A Standard ICM, low current
802.3at (Type 2) 25.5W ~0.6A ICM rated for PoE+
802.3bt Type 3 51W ~0.6A per mode (2 modes) ICM with dual-mode center taps
802.3bt Type 4 71W ~0.96A per mode (2 modes) ICM with high-current center taps, thermal-rated

At 90W (Type 4), each transformer winding carries nearly 1A of DC current. If the transformer core is undersized, magnetic saturation occurs, causing signal distortion, overheating, and potential fire. VITALCONN's PoE++ ICM RJ45 connectors use oversized ferrite cores and thermally-rated wire to handle the full 90W without saturation.

EMI Performance: Why Magnetics Matter

The common-mode choke inside an ICM RJ45 is critical for EMI compliance. Without it, common-mode noise from the PHY couples directly onto the cable, which acts as an antenna, radiating emissions that can exceed FCC Class A limits. VITALCONN's ICM RJ45 connectors include common-mode chokes on every pair, providing 25-35 dB of common-mode rejection from 30 MHz to 500 MHz. This is essential for passing FCC/CISPR radiated emissions tests, especially for 10GBase-T where the signal spectrum extends to 500 MHz.

VITALCONN Magnetic RJ45 (ICM) Product Line

VITALCONN manufactures 163+ ICM RJ45 models, making us one of the most comprehensive ICM suppliers in the industry. Our magnetic RJ45 product line covers:

Category Models Key Specs
10/100Base-T ICM 30+ 1:1 CT, 1500VAC, 2-pair PoE
1000Base-T (1G) ICM 50+ 1:1 CT, 1500-3000VAC, PoE/PoE+/PoE++
2.5G/5GBase-T ICM 15+ 1:1 CT, 1500VAC, low insertion loss
10GBase-T ICM 10+ 1:1 CT, 5000VAC, enhanced EMI shield
Stacked (2xN) ICM 30+ 2x1 to 2x8, shared/independent magnetics
Non-Magnetic RJ45 20+ For designs with external magnetics

Why choose VITALCONN ICM?

  • Full speed range: 10/100M to 10GBase-T
  • Full PoE range: 802.3af (15.4W) to 802.3bt Type 4 (90W)
  • Hi-Pot isolation: 1500-5000 VAC
  • Operating temperature: -40°C to +85°C (industrial)
  • Common-mode rejection: ≥ 25-35 dB (30-500 MHz)
  • ARP cross-reference: 26 replacements for Pulse, BelFuse, TE, Molex, Amphenol
  • Custom gold plating: flash to 50 microinches
Tip: VITALCONN's ARP platform provides 26 pin-to-pin cross-reference replacements for Pulse, BelFuse, TE, Molex, and Amphenol ICM RJ45 connectors. Benefits include 30-40% cost savings and 2-4 week lead times vs. 12-24 weeks for major brands.

Frequently Asked Questions (FAQ)

Do I need a magnetic RJ45 for PoE?

Yes. PoE requires center-tapped transformers to inject DC power onto the cable. A non-magnetic RJ45 does not have transformers, so it cannot support PoE. You would need external center-tapped magnetics on the PCB. Using an ICM (integrated magnetic) RJ45 simplifies this, as the center taps are built in.

Can I use a non-magnetic RJ45 with external magnetics?

Yes. Some designs use a non-magnetic RJ45 connector with discrete transformers and common-mode chokes placed on the PCB. This is common in legacy designs or when custom magnetic specifications are needed. However, most new designs use ICM for simplified layout and guaranteed compliance.

What is the turns ratio for RJ45 magnetics?

The standard turns ratio for Ethernet magnetics is 1CT:1CT (1 center-tapped to 1 center-tapped), which provides a 1:1 impedance ratio matching the 100-ohm PHY to the 100-ohm cable. Some specialized applications use 1CT:1.41CT or other ratios for impedance matching to non-standard cable impedances.

What is Hi-Pot isolation in ICM RJ45?

Hi-Pot (high-potential) isolation is the voltage the transformer can withstand between the primary (PHY side) and secondary (cable side) windings without breakdown. The minimum per IEC 60603-7 is 1500 VAC RMS. Industrial and medical applications may require 3000-5000 VAC. VITALCONN offers ICM models with isolation up to 5000 VAC.

Can I use a 10/100M ICM for Gigabit Ethernet?

No. A 10/100M ICM only has magnetics on 2 pairs (pins 1-2 and 3-6). Gigabit Ethernet (1000Base-T) requires magnetics on all 4 pairs. You need a Gigabit-rated ICM with 4-pair magnetics. Using a 10/100M ICM on a Gigabit port will prevent the link from establishing.

How does VITALCONN's ICM compare to Pulse or BelFuse?

VITALCONN's ARP platform provides 26 pin-to-pin cross-reference replacements for Pulse Electronics, BelFuse, TE Connectivity, Molex, and Amphenol RJ45 connectors. Our ICMs offer equivalent electrical specifications with 30-40% cost savings and 2-4 week lead times versus 12-24 weeks for major brands. Contact sales@vitalconn.com for a cross-reference.

Need Magnetic RJ45 (ICM) Connectors?

VITALCONN manufactures 163+ ICM RJ45 models with ISO 9001 certified quality.
Request free samples or a custom quote.

Understanding the RJ45 pinout is essential for anyone working with Ethernet networking, from PCB design engineers to cable installation technicians. The RJ45 connector uses an 8-position, 8-contact (8P8C) modular jack, and its pinout determines how data signals travel between networked devices. Two wiring standards govern this pinout: T568A and T568B. While both support the same Ethernet speeds, the difference lies in the color-coded wire-to-pin assignment. This guide provides a complete RJ45 wiring diagram, explains the T568A vs T568B distinction, and covers crossover vs straight-through cable configurations — all critical knowledge for designing and maintaining reliable network connections.

Whether you are designing a network switch motherboard, specifying connectors for an industrial gateway, or wiring a data center rack, getting the RJ45 pinout right is non-negotiable. A single swapped pair can cause intermittent connectivity, signal degradation, or complete link failure. As Ethernet speeds increase from 1G to 10G and beyond, correct pinout and wire pair twisting become even more critical for maintaining signal integrity.

This guide is written for hardware engineers, PCB designers, and network technicians who need authoritative, practical information about RJ45 pinout standards. VITALCONN Electronics manufactures RJ45 connectors with integrated magnetics and discrete options — see our Ultimate Guide to RJ45 Connectors for a complete product overview — and this guide draws on our engineering team's field experience to address the most common pinout questions.

RJ45 Pinout Diagram: T568A vs T568B Color Code Assignments

The RJ45 connector has 8 pins, numbered 1 through 8 when looking at the connector from the front (contact side facing you, tab pointing down). Each pin is assigned a specific wire color under the TIA/EIA-568 standard. Below is the complete RJ45 pinout for both T568A and T568B:

Pin # T568A Color T568B Color Signal (T568B) Pair #
1 White/Green White/Orange TX+ (Transmit +) Pair 2
2 Green Orange TX- (Transmit -) Pair 2
3 White/Orange White/Green RX+ (Receive +) Pair 3
4 Blue Blue Blue Pair (PoE+) Pair 1
5 White/Blue White/Blue Blue Pair (PoE-) Pair 1
6 Orange Green RX- (Receive -) Pair 3
7 White/Brown White/Brown Brown Pair (PoE+) Pair 4
8 Brown Brown Brown Pair (PoE-) Pair 4

Key observations from this pinout table:

  • Pins 1 and 2 are always a differential pair (transmit in T568B)
  • Pins 3 and 6 are always a differential pair (receive in T568B)
  • Pins 4, 5, 7, and 8 are used for Power over Ethernet (PoE) in Mode B (phantom power on spare pairs)
  • The only difference between T568A and T568B is that the Orange and Green pairs are swapped

T568A vs T568B: Which Standard Should You Use?

The difference between T568A and T568B is purely the color-to-pin assignment. Electrically, both standards carry Ethernet signals identically — the data reaches the same pins on the RJ45 connector regardless of which color code is used. The critical rule is consistency: both ends of a straight-through cable must use the same standard.

T568B is the most commonly used standard in the United States and in commercial installations worldwide. T568A is more common in residential wiring and is the preferred standard for U.S. government contracts. From a technical standpoint, there is no performance difference between the two.

Aspect T568A T568B
Pair 2 (Pins 1,2) Green pair Orange pair
Pair 3 (Pins 3,6) Orange pair Green pair
Performance Identical to T568B Identical to T568A
Common Usage Residential, U.S. government Commercial, most common globally
Standard Origin Original AT&T 258A color code ANSI/TIA-568 commercial standard
Compatibility Compatible with T568B (both ends must match) Compatible with T568A (both ends must match)
⚠ Important: When designing PCBs with RJ45 connectors, the pinout on the PCB layout must match the cable standard you intend to use. Most RJ45 jacks are wired for T568B by default, but the PCB trace routing is what ultimately determines which standard your board follows. Always document the chosen standard in your design files.

RJ45 Wiring Diagram: Straight-Through vs Crossover Cables

Two cable types use the RJ45 pinout: straight-through and crossover. Understanding the difference is critical for proper network connectivity.

A straight-through cable uses the same wiring standard (either T568A or T568B) on both ends. This is the standard cable for connecting different device types — for example, a computer to a switch, or a router to a switch.

A crossover cable uses T568A on one end and T568B on the other. This swaps the transmit and receive pairs, allowing two devices of the same type (such as two computers or two switches) to communicate directly without an intermediary device.

Cable Type End A End B Typical Use Case
Straight-Through T568B T568B PC to switch, router to switch
Straight-Through T568A T568A PC to switch (less common)
Crossover T568A T568B PC to PC, switch to switch (legacy)
💡 Note: Modern networking equipment typically supports Auto-MDIX, which automatically detects the cable type and adjusts transmit/receive internally. This has made crossover cables largely obsolete for most applications. However, on PCB-level designs and embedded systems, Auto-MDIX support is not always guaranteed, so understanding the pinout remains essential.

RJ45 Pinout and Power over Ethernet (PoE): What Engineers Need to Know

The RJ45 pinout plays a critical role in Power over Ethernet (PoE) applications. PoE delivers DC power over the same Ethernet cable that carries data, and it uses specific pin pairs depending on the PoE mode:

PoE Standard Power Rating PoE Mode Pins Used for Power
IEEE 802.3af 15.4W Mode A (phantom power) Pins 1-2, 3-6 (same as data)
IEEE 802.3af 15.4W Mode B (spare pairs) Pins 4-5, 7-8
IEEE 802.3at (PoE+) 30W Mode A or Mode B Same pin assignments as af
IEEE 802.3bt Type 3 60W Mode A or Mode B Pins 1-2, 3-6 and/or 4-5, 7-8
IEEE 802.3bt Type 4 90W Mode A or Mode B All 4 pairs (4-pair PoE)

For PCB designers, the RJ45 connector selected must be rated for the intended PoE standard. Connectors carrying PoE must handle higher current per contact (up to 960mA for 802.3bt Type 4), which affects contact plating thickness, PCB trace width, and thermal management. For detailed PoE connector selection guidance, see our PoE RJ45 connector guide covering current ratings, thermal considerations, and connector selection criteria.

RJ45 Wiring Diagram and Signal Integrity at Higher Speeds

At Gigabit Ethernet (1000BASE-T) and above, the RJ45 pinout becomes more than just wire color matching — it directly impacts signal integrity. At these speeds, all four twisted pairs are used bidirectionally, and maintaining pair twisting as close to the connector as possible is critical. For a deeper dive into the magnetics that make this possible, see our LAN transformer guide.

For 10GBASE-T (10 Gigabit Ethernet over copper), the pinout requirements are even more stringent:

  • Pair untwist length inside the connector should not exceed 13mm (0.5 inch)
  • Shielded RJ45 connectors with metal housings are strongly recommended for 10G applications
  • PCB trace impedance should be controlled to 100 ohms differential
  • Crosstalk performance must meet or exceed Category 6A specifications

For high-speed Ethernet connector selection guidance including 10G RJ45 options, refer to our RJ45 connector buying guide which covers shielding, magnetics integration, and speed rating considerations. If you are also weighing different connector form factors, our RJ45 vs RJ11 comparison covers the key differences.

Common RJ45 Pinout Mistakes and How to Avoid Them

Even experienced engineers and technicians make pinout errors. Here are the most common mistakes and their consequences:

Mistake Symptom Solution
Mixing T568A and T568B on straight-through cable No link or intermittent connectivity Verify both ends use the same standard; use a cable tester
Splitting Pair 3 (pins 3 and 6 on different wire pairs) Crosstalk, reduced speed, link errors Ensure pins 3 and 6 use wires from the same twisted pair
Untwisting pairs too far from connector Signal degradation at Gigabit speeds Maintain twist to within 13mm of the termination point
Wrong PoE pin assignment in PCB layout PoE device fails to power or connector overheats Follow IEEE 802.3 pin assignments; verify current ratings
Using unshielded connector for 10G application EMI interference, packet loss Use shielded RJ45 with metal EMI housing for 10GBASE-T

Frequently Asked Questions (FAQ)

What is the difference between T568A and T568B?
T568A and T568B are two wiring standards for RJ45 connectors. The only difference is the color-to-pin assignment: T568A uses the green pair on pins 1-2 and orange pair on pins 3-6, while T568B reverses this (orange on 1-2, green on 3-6). Electrically, both perform identically. The key rule is to use the same standard on both ends of a straight-through cable.
Can I mix T568A and T568B on the same cable?
Only if you intentionally want a crossover cable. If you use T568A on one end and T568B on the other, you create a crossover cable that swaps transmit and receive pairs. This was used for same-device connections (PC-to-PC, switch-to-switch) before Auto-MDIX became standard. For normal straight-through cables, both ends must match.
Which RJ45 pinout standard is more common?
T568B is the most commonly used standard globally, especially in commercial installations and data centers. T568A is preferred for U.S. residential wiring and government contracts. Both are formally recognized by ANSI/TIA-568. Choose one standard and use it consistently across your entire installation.
Does the RJ45 pinout affect PoE power delivery?
Yes. PoE delivers power over specific pin pairs. Mode A (phantom power) uses the same pins as data (1-2, 3-6), while Mode B uses spare pairs (4-5, 7-8). The pinout must follow IEEE 802.3 standards to ensure correct power delivery. For 4-pair PoE (802.3bt Type 4, 90W), all four pairs carry power simultaneously.
What is pin 1 on an RJ45 connector?
Pin 1 is the leftmost pin when looking at the RJ45 connector from the front (contact side facing you, tab pointing down). In T568B wiring, pin 1 is assigned the White/Orange wire and carries the TX+ (Transmit Positive) signal. In T568A, pin 1 is assigned the White/Green wire.
Ready to Select the Right RJ45 Connector?
Explore VITALCONN's full range of RJ45 connectors with integrated magnetics and discrete options, or request free samples for your next project.
Explore RJ45 Connectors View Cross-Reference Table